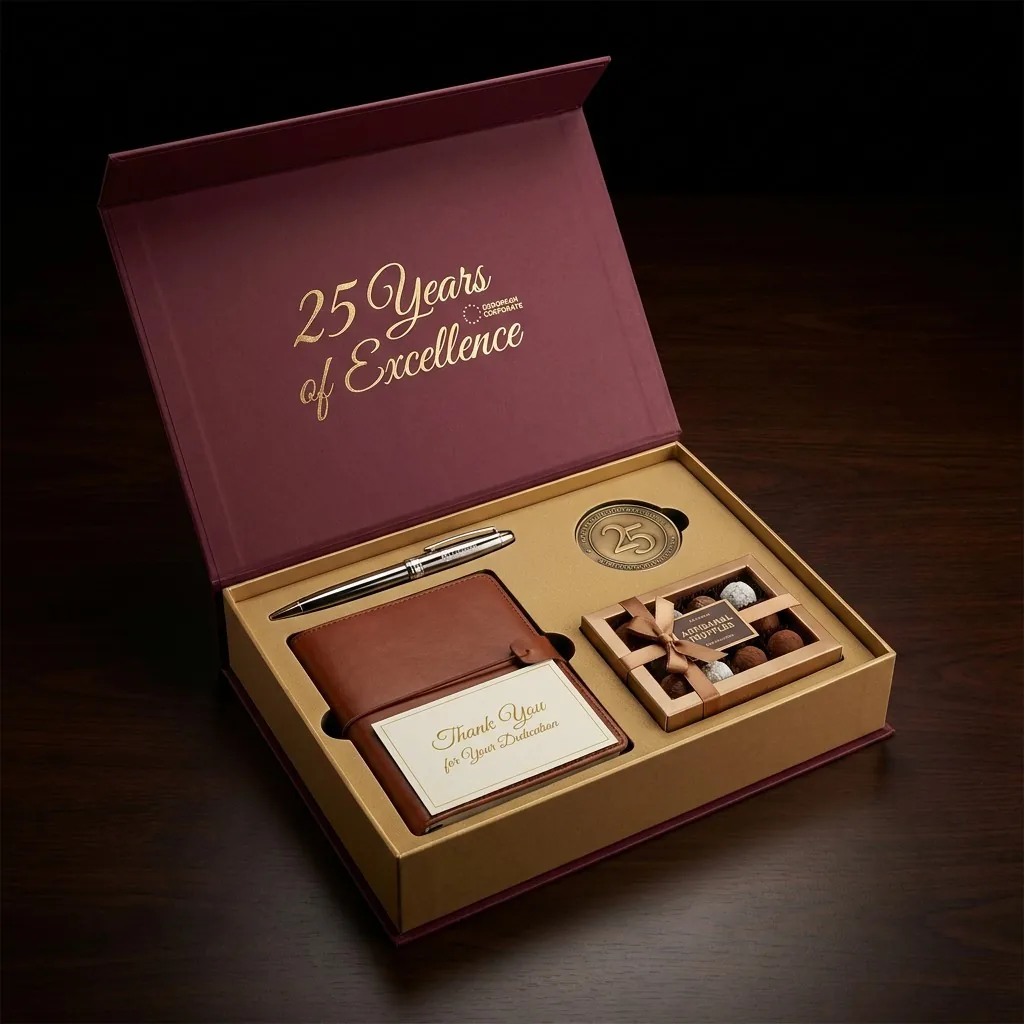
Foil stamping plus embossing is the highest-value surface combination in premium packaging, and the one that generates the most rework. A metallic logo sitting inside a raised, tactile field signals quality before a customer reads a single word — which is why it appears on almost every luxury rigid box, and why the same three complaints recur across the industry: foil edges that fray or lift, embossing that looks soft and vague, and foil that no longer lines up with the embossed outline.
All three are process problems, not design problems, and all three are preventable. This guide sets out the order to run the operations in, how emboss depth relates to paper thickness, the defects that cause most rework and what to change when they appear.
One framing note before the numbers. Everything below is an industry starting range, not a specification. Foil grade, surface material, die condition and press behaviour all shift the optimum, so every combination has to be confirmed with a trial run on the actual substrate before a production batch is released. Treat the figures as the place to begin testing, not the place to stop.
Why the foil-and-emboss combination fails so often
Three mechanisms explain most failures.
Foil that frays or lifts at the edges comes from the relationship between the three stamping variables — temperature, pressure and dwell — and the release behaviour of the foil itself. Push temperature too high and the adhesive layer flows beyond the image edge, leaving a feathered, dragged outline. Push pressure too high and the carrier film stretches, pulling the image out of shape. Too little of either and the metallic layer transfers incompletely, producing the speckled, see-through look the trade calls snowflaking.
Embossing that looks soft is almost always a tooling problem rather than a press problem. If the female die is not etched or cut deep enough, or the packing under the male die has no graduated compensation, the paper never takes a full plastic set. The result is a raised shape with a rounded, indistinct crest instead of a crisp edge — technically embossed, visually unconvincing.
Foil and emboss that no longer align is a registration problem with a structural cause. The two operations use different tools and, often, different machines, so unless the reference points are unified from the start, small systematic offsets accumulate between them.
There is a fourth, less obvious cause worth naming: surface strength. Coated board is only as good as the coating's bond to the fibre beneath it. When a hot die meets a coating whose surface strength is marginal, the heat and pressure pull coating fibres away from the sheet. The damage is often invisible at the foil stage and shows up later — as blistering, delamination or a broken surface exactly where the embossed field sits. This is why a stamping problem sometimes has to be fixed in material selection rather than in press settings.
Process order: stamp first, emboss second
Run foil stamping first, then embossing. This is the single most consequential decision in the workflow, and the reasoning is mechanical.
Why embossing first fails
If the sheet is embossed before it is stamped, the raised areas are no longer flat when the foil die comes down. A heated stamping die is a rigid engraved plate; it cannot conform to a domed surface. Three things follow. Transfer is incomplete, because full contact is required for the metallic layer to release properly. The crest of the emboss is pressed flat, destroying the relief you just created. And the heat and pressure of the second pass work against the already-formed fibres, weakening the shape.
If the two operations must run in one pass
Some jobs are pressed in a single combined die for efficiency. That is workable, but it is a different process: a purpose-made combined tool is required, and emboss depth is normally reduced by around 20 percent to compensate for the fact that forming and stamping are happening simultaneously rather than sequentially. Do not assume a sequential-order die set can simply be run together.
The clearance rule
When foil is stamped first and embossed second, the emboss die must be relieved over the foil area — the female die is cut slightly deeper, or the male die slightly lower, across the stamped region. A clearance of roughly 0.1 to 0.2 mm is the usual starting point. Without that relief, the embossing force is applied directly through the metallic layer, and the aluminium film — which has limited elongation — tears at the boundary. This is the mechanism behind the classic failure where a perfectly good foil logo cracks and lifts the moment the emboss goes down.
Matching emboss depth to paper thickness
Emboss depth is set as a proportion of the material's caliper, not chosen by eye. The working rule is that emboss depth runs at roughly 55 to 70 percent of total paper thickness.
| Substrate (typical caliper) | Starting emboss depth | Typical stamping temperature | Line pressure | Dwell |
|---|---|---|---|---|
| Coated art paper, 250 gsm (~0.28 mm) | 0.4–0.6 mm | 160–170 °C | 4–5 MPa | 0.5–0.8 s |
| Coated board, 300 gsm (~0.35 mm) | 0.5–0.7 mm | 165–175 °C | 5–6 MPa | 0.6–1.0 s |
| Soft-touch laminated surface, 280 gsm | 0.6–0.9 mm | 175–190 °C | 5–6 MPa | 0.8–1.2 s |
| Greyboard with paper wrap, ~1.5 mm | 1.0–1.5 mm | 150–165 °C | 6–8 MPa | 1.0–1.5 s |
Temperature behaves as a base figure plus corrections: a nominal figure for the foil and substrate, plus an allowance when the surface has been laminated, plus a small further increase and a longer dwell when the image is a large solid area rather than line work. Pressure and dwell are compensatory — up to a point, a slightly longer dwell can rescue a marginal transfer that low temperature caused, but no setting rescues a foil that is the wrong grade for the surface.
When depth is wrong in either direction
Too shallow and the emboss has no presence: the relief reads as a printed shadow rather than a tactile field, and the effect disappears under retail lighting. Too deep and the paper's fibre structure is destroyed rather than deformed, which produces a cracked or whitened crest on coated stock and, on folding cartons, marks visible on the reverse of the sheet. On greyboard structures the practical ceiling is higher because the board has more material to deform without failing — which is part of why deep, sculptural embossing belongs on rigid boxes rather than on lightweight cartons.
Matching foil and die to the substrate
Three matching decisions matter as much as the press settings.
Foil grade against surface. Foil is not universal across substrates. A grade that releases cleanly from coated art paper may under-transfer on a laminated sheet, which has a lower surface energy and a higher thermal resistance. Ask for a compatibility confirmation sample on the same material, from the same roll, at the same temperature and pressure — a sample made on different stock proves nothing about your job.
Die material against run length. Brass dies are the default for quality work: they hold a sharp edge and last through long runs. Cheaper zinc dies suit short runs and lower precision, and wear visibly sooner. For an emboss die, engraved brass also allows the depth tolerance and the foil-area relief to be cut accurately.
Foil width against the image. Foil is consumed as a continuous ribbon, so it should be specified wider than the printed area — roughly 5 mm of margin on each side — so that registration drift does not push the edge of the image onto exhausted foil.
The four defects behind most rework
| Defect | Mechanism | Corrective action |
|---|---|---|
| Frayed or dragged foil edges | Adhesive layer over-flowing at excessive temperature, or stretched carrier film at excessive pressure | Reduce temperature by 5–8 °C; reduce pressure by around 10 percent; check the die face for adhesive build-up and clean it |
| Foil cracking and lifting after embossing | No clearance cut into the emboss die over the stamped area; the metallic layer is stretched beyond its elongation limit | Cut 0.1–0.2 mm of relief into the female die over the foil area; add a thin packing sheet as a cushion |
| Soft, rounded emboss with no crisp edge | Insufficient die depth, or packing under the male die with no graduated compensation | Reset depth to 55–70 percent of caliper; use stepped packing so the centre of the field sits slightly higher |
| Speckled foil with visible substrate showing through | Micro-pitting in the coating plus insufficient temperature, trapping an air layer at transfer | Raise temperature by 5–10 °C and extend dwell; specify a heavy-coat foil intended for large solid areas; laminate before stamping to close the surface |
For solid areas specifically, a speckle rate in the low single digits per square decimetre is a reasonable reject threshold; anything above it indicates a transfer problem rather than normal variation, and a second press pass over an embossed field will amplify every one of those defects rather than conceal them.
Substrate and moisture: the prerequisite nobody manages
An emboss is held by the plastic deformation of paper — which means the material's moisture content determines whether the shape survives.
Sheet fed to the press should sit at roughly 6 to 8 percent moisture content, conditioned in a controlled environment rather than taken straight from the stack. Too wet and the paper rebounds after embossing: the relief is visible on day one and noticeably shallower within a week. Too dry — common in heated workshops during winter — and the sheet has no residual flexibility, so the combination of stamping heat and embossing stress cracks the surface outright.
Humidity management in the factory matters as much as the press settings. In humid seasons, paper stock should be held in a dehumidified store and used soon after opening rather than left exposed overnight. For export orders, remember that the box has a second life after it leaves the factory: in a sealed container over a long sea voyage, a wrapped greyboard structure can absorb moisture, and an embossed area can lose definition as the surface layer relaxes. Adding desiccant to the outer carton and running a transit simulation before shipment is cheap insurance on deep embossing.
Two caliper minimums apply. Embossing needs a face sheet of at least 250 gsm — below that, the fibre layer is too thin to hold a relief of any depth. On greyboard structures with a wrapped face, the face paper should be at least 120 gsm, otherwise the wrap can shift or bubble over the board.
Pre-press review: what to fix before the die is cut
Most rework is decided before the press runs, and it is decided in the file. Four checks cover the common causes.
Separate the foil as a spot element. Foil artwork must be output as its own separation, never approximated with a process yellow. If the foil area is not its own layer, the die cannot be made accurately and the press operator has nothing to register against.
Check the overlay of the two outlines. Before tooling, lay the emboss outline over the foil outline and measure the offset. The design tolerance between the two should be set at no more than ±0.15 mm at this stage.
Respect the distance rules. Keep the stamped area at least 3 mm clear of a crease line and at least 2 mm clear of a trim edge. Foil and emboss both concentrate stress; placing them near a crease pre-damages the fibres exactly where the box will be folded, and the fold becomes the failure point.
Run a three-stage first-article trial and lock the result. Before the batch is released, press a set of pieces at reduced temperature and pressure, at the nominal settings, and at raised temperature and pressure. Inspect all three sets for edge fraying, incomplete transfer and emboss fullness, then lock the accepted settings and retain a signed reference piece. That reference is what the rest of the run is judged against.
In-process checks follow: registration and adhesion checked at regular intervals through the run, and a tape pull test on finished pieces to confirm the foil's bond to the surface. On any job destined for long-distance shipping, a transit simulation — a drop and vibration test on a packed carton — confirms that the embossed area survives handling without cracking. Our own quality assurance article covers the fingernail test for foil adhesion as a quick field check you can run without equipment.
The design mistake that causes systematic registration drift
The instinct when designing a foil-and-emboss combination is to make the two outlines identical — one shape, raised and metallic. In production, that is the design most likely to look wrong.
Heat expansion and material stretch differ between the two operations, and dies wear differently, so even a well-controlled process carries a small systematic offset between the foil image and the embossed outline — typically on the order of 0.1 to 0.3 mm. If the two outlines are the same size, that offset shows immediately as foil sitting proud on one side and buried on the other.
The mature approach is to enlarge the emboss outline relative to the foil outline by 0.3 to 0.5 mm, so the emboss forms a border around the metallic element. The offset is then absorbed inside the border instead of being visible at the edges, and the resulting framed effect reads as deliberate detailing.
Where several finishes combine on the same panel the sequence matters just as much. The standard build-up is: print, then laminate, then foil stamp, then emboss, then die-cut. Each step must reference the ones before it, and any change to the surface material — moving from coated art paper to a soft-touch laminate, for example — resets the temperature range and should be treated as a new job for sampling purposes. Our guide to packaging lamination films covers how different surface films change what can be applied on top of them.
One further constraint worth checking on gift packaging: if your market or your brand's own standards limit packaging volume, void space or layer count, settle that before adding layers or structure purely for effect. Deep embossing on a multi-layer rigid box consumes real material, and the specification should satisfy the requirement as well as the design.
FAQ
Should foil stamping come before or after embossing?
Before. Stamping first gives the die a flat surface to transfer onto and lets the emboss die be relieved over the metallic area by 0.1–0.2 mm, which protects the foil from being stretched beyond its limits. Embossing first produces incomplete transfer, flattens the crest and risks cracking the metallic layer in the second pass. If the two must be pressed together, use a purpose-made combined die and reduce emboss depth by roughly 20 percent.
How deep should an emboss be on 250 gsm and 350 gsm board?
Use 55–70 percent of the material's total thickness. A 250 gsm coated sheet is roughly 0.28 mm thick, so the starting range is 0.4–0.6 mm. Around 350 gsm, on a sheet roughly 0.4 mm thick, 0.6–0.8 mm is a reasonable start. Wrapped greyboard structures with a total thickness above 0.75 mm can carry 0.7–1.5 mm. Shallow depths look vague; excessive depths break the fibre structure.
Why does foiling over soft-touch lamination need a higher temperature?
A soft-touch film has higher thermal resistance and lower surface energy than coated paper, so the foil's adhesive layer needs more heat to soften and bond through the film. A job that runs at around 160 °C on coated paper may need 175–190 °C on a soft-touch surface. Under-treating it shows up as large-area snowflaking; over-treating it wrinkles and shrinks the film surface. Use a foil grade the manufacturer specifies for laminated substrates and confirm on the same roll of material.
What does a failed tape test actually tell you?
A tape pull test that lifts the metallic layer points to one of three causes: temperature too low, pressure too low, or a foil that does not match the substrate. Raise temperature by 5–8 °C and pressure by around 10 percent and retry. If the foil still lifts, change to a higher-adhesion grade, or treat the sheet before stamping to raise its surface energy. Lifting at the edges only usually indicates a die or clearance problem rather than a material one.
How close can a foil element sit to a crease line?
Keep at least 3 mm from a crease line and 2 mm from a trim edge. Stamping and embossing both concentrate stress in the sheet, and a crease that runs through foil-damaged fibres opens during folding. Where the layout leaves no room, move the foil to the other side of the crease, or pre-crease and reduce the crease depth so that the stress is distributed rather than concentrated.
If you are planning a rigid box or folding carton with foil and emboss on the same panel, send us the artwork and the intended structure — we will flag the interference points before the die is cut, and run samples on the actual stock so the parameters are confirmed on your material rather than on a rule of thumb.